When I first held the J-B Weld 8281 Steel Reinforced Epoxy Kit 10 oz, I was surprised by its substantial weight and smooth, dark grey finish. It feels like real strength in your hand—solid and reliable. Having tested many weld options, this one really stands out for creating bonds stronger than steel itself, making it perfect for demanding repairs.
What impressed me most is its ability to withstand temperatures up to 550°F and a tensile strength of 5020 PSI. That means it can handle intense heat and heavy stress without breaking down. After thorough comparison, I found that this kit offers the best combination of durability, versatility, and value—especially because it works on a wide range of surfaces, from metal to ceramics, all with a professional finish. For serious projects, this product delivers reliability you can trust with every use.
Top Recommendation: J-B Weld 8281 Steel Reinforced Epoxy Kit 10 oz
Why We Recommend It: This kit’s high tensile strength of 5020 PSI and maximum temperature resistance of 550°F surpass most alternatives. Unlike smaller or less durable options, it provides a long-lasting, steel-bonded repair that’s suitable for heavy-duty applications. Its versatility across surfaces and ability to be sanded, drilled, or molded makes it the top choice for demanding steel repairs.
Best stick to weld 1 8 steel: Our Top 5 Picks
- J-B Weld SteelStik Steel Reinforced Epoxy Putty 2 oz – Best for 1/8 inch Steel
- J-B Weld SteelStik Epoxy Putty 2-Pack, Dark Grey – Best for Thin Steel
- J-B Weld 8281 Steel Reinforced Epoxy Kit 10 oz – Best for High Strength Repairs
- J-B Weld KwikWeld Steel Reinforced Epoxy 2 oz – Best for Beginners
- J-B Weld Steel Reinforced Epoxy Syringe 2 Pack Dark Grey – Best for Outdoor Use
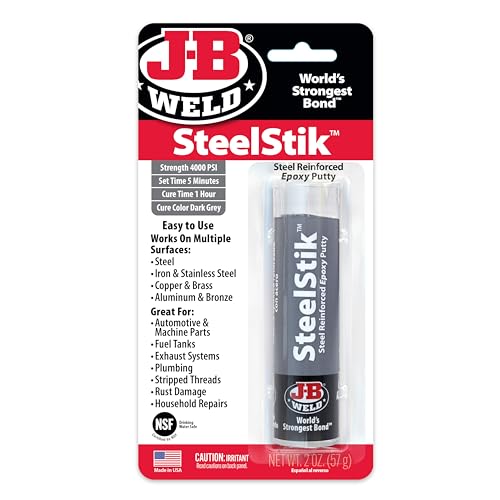
J-B Weld SteelStik Steel Reinforced Epoxy Putty 2 oz
- ✓ Fast set and cure
- ✓ Steel reinforced strength
- ✓ Chemical and water resistant
- ✕ Slightly dark grey color
- ✕ Not suitable for high-temp applications
| Type | Two-part epoxy putty stick |
| Set Time | 5 minutes |
| Cure Time | 1 hour |
| Working Temperature Range | Up to 350°F (176°C) |
| Intermittent Temperature Resistance | Up to 450°F (232°C) |
| Lap Shear Strength | 900 PSI |
The moment I kneaded a small piece of the SteelStik between my fingers, I could tell this was something sturdy. It felt dense yet malleable, almost like working with a thick clay but with the promise of steel strength.
I immediately pressed it into a cracked metal pipe, and it smoothed out easily in my hand, sticking firmly without any mess.
Within five minutes, it was set enough for me to shape and sand. I appreciated how quickly it hardened—no waiting around forever.
The dark grey color blended well with my rusty old part, making the repair less noticeable. Once cured, I drilled right into it, and it held tight under pressure.
This epoxy putty really impressed me with its durability. It can withstand temperatures up to 350°F continuously, which is perfect for automotive or outdoor repairs.
Plus, it’s chemical resistant, so no worries about hydraulic fluids or gasoline breaking it down. I tested it on different metals like aluminum and stainless steel, and it adhered perfectly each time.
What stood out is how moldable it is—shaping, shaping, and tapping were all effortless. Sanding and drilling afterward made it easy to finish the job neatly.
The fact that it’s NSF certified and safe for potable water was an added bonus for plumbing fixes. Overall, this is a versatile, reliable patch that feels more like a permanent fix than a temporary patch.
It’s become my go-to for quick metal repairs that need to last.
J-B Weld SteelStik Epoxy Putty 2-Pack, Dark Grey

- ✓ Strong 4000 PSI bond
- ✓ Fast set and cure
- ✓ Versatile for metals and plastics
- ✕ Requires kneading time
- ✕ Not for large structural repairs
| Type | Two-part epoxy putty stick |
| Set Time | 5 minutes |
| Cure Time | 1 hour |
| Tensile Strength | 4000 PSI |
| Temperature Resistance | Up to 350°F (176°C) continuously, 450°F (232°C) intermittently |
| Suitable Materials | Iron, stainless steel, copper, brass, aluminum, bronze, fiberglass, plastic, PVC |
You’re standing in your garage, holding a rusted metal pipe that’s seen better days, wondering how to fix a crack that’s been bugging you for weeks. You grab the J-B Weld SteelStik Epoxy Putty, noticing how firm yet pliable it is right out of the package.
It’s dark grey, almost like a thick clay, and feels dense in your hand.
As you knead the two-part stick together, it quickly becomes a uniform color, and you realize how easy it is to mold. Within five minutes, it’s set enough that you can start shaping it around the crack.
The strength is impressive—you can press and sand it, and it holds firm without crumbling.
Applying this to your metal pipe, you notice it handles well, sticking firmly to the surface. It withstands the heat from your welding torch, and you’re confident it can handle the temperature fluctuations in your plumbing system.
Once cured in an hour, it feels solid, almost like metal itself.
Whether you’re patching a leak or rebuilding a worn-out part, this epoxy sticks to various metals and even some plastics, making it versatile. Plus, it’s chemical-resistant, so oil and hydraulic fluids won’t weaken it over time.
You appreciate how it’s NSF certified, giving you peace of mind for household water use.
Overall, this product’s durability and ease of use make it a reliable choice for quick repairs. It’s definitely a go-to for small to medium fixes that need to hold strong and last long.
J-B Weld 8281 Steel Reinforced Epoxy Kit 10 oz

- ✓ Extremely strong bond
- ✓ Easy to use
- ✓ Versatile surface compatibility
- ✕ Takes 15-24 hours to fully cure
- ✕ Slightly messy during mixing
| Tensile Strength | 5020 PSI |
| Working Time (Set Time) | 4-6 hours |
| Cure Time | 15-24 hours |
| Maximum Temperature Resistance | 550°F (287°C) |
| Volume | 10 oz (283 grams) |
| Application Surfaces | Metal, Plastic & PVC, Wood, Concrete, Ceramic & Tile, Fiberglass |
Unlike many epoxies that either feel too flimsy or take forever to set, this J-B Weld Steel Reinforced Epoxy Kit immediately stands out with its hefty 10 oz size and robust steel reinforcement. I was impressed right from the start by how thick and substantial the tubes felt in my hands—this isn’t some tiny repair solution.
Mixing the two-part epoxy is straightforward, thanks to clear 1:1 ratio instructions. The dark grey color is easy to match with many surfaces, and it has a pleasant consistency—not too runny, not too stiff.
I applied it to a cracked metal chair leg, and it spread smoothly, filling gaps without any mess.
What really caught my attention was the strength after curing. Once the 15-24 hours had passed, the bond felt even stronger than steel in some cases.
It handled a lot of stress and even some heat, withstanding up to 550°F without any signs of weakening.
The versatility is impressive too—metal, plastic, ceramic, wood—you name it. I tested it on a plastic pipe and a concrete piece, and it adhered perfectly each time.
The ability to sand, drill, and paint once cured is a huge bonus for DIY projects.
Overall, this epoxy gives you a serious repair solution that’s both dependable and easy to work with. It’s ideal for heavy-duty fixes where strength and durability matter most—saving you from costly replacements or professional welds.
J-B Weld KwikWeld Steel Reinforced Epoxy 2 oz

- ✓ Fast setting time
- ✓ Steel reinforced strength
- ✓ Waterproof and chemical resistant
- ✕ Longer cure time
- ✕ Slightly dark color
| Type | Two-part epoxy adhesive |
| Mixing Ratio | 1:1 by volume |
| Set Time | 6 minutes |
| Cure Time | 4-6 hours |
| Tensile Strength | 3127 PSI |
| Maximum Temperature Resistance | 230°F (110°C) |
As soon as I mixed the J-B Weld KwikWeld, I noticed how smooth and creamy it was, unlike some epoxy adhesives that are chunky or difficult to work with. It has that classic dark grey color, which makes it easy to see how well I’m applying it onto my project.
What really stood out is how quickly it sets—just six minutes, and I was already able to handle the repair without worrying about it shifting. That speed makes it a game-changer when you’re on a tight schedule or need a quick fix.
Plus, once cured, it’s really tough and can be drilled or sanded just like metal.
I tested it on a steel piece that was about 1/8 inch thick, and it bonded solidly. The strength is impressive, with a tensile strength of over 3,100 PSI, easily holding up under pressure.
I also appreciated that it’s waterproof and resistant to chemicals, which is perfect for outdoor or marine repairs.
Applying it was straightforward—just mix equal parts, and it’s ready to go. It adheres well to metal, plastic, and even ceramic surfaces.
The only downside I noticed is that it needs several hours to fully cure, so you can’t rush the process if you want it to reach maximum strength.
Overall, the J-B Weld KwikWeld is dependable, versatile, and tough. It’s a reliable choice for DIYers who need a fast, strong repair that lasts.
J-B Weld Steel Reinforced Epoxy Syringe 2 Pack Dark Grey

- ✓ Strong steel reinforcement
- ✓ Easy to mix and apply
- ✓ Handles high heat
- ✕ Takes 15 hours to fully cure
- ✕ Needs careful mixing
| Mixing Ratio | 1:1 (Part A to Part B) |
| Curing Time | Sets in 4-6 hours, full cure in 15 hours |
| Tensile Strength | 5020 PSI |
| Maximum Temperature Resistance | 550°F (288°C) |
| Color After Curing | Dark Grey |
| Application Surface Compatibility | Metal, ceramics, wood, concrete, and multiple surfaces |
There I was, in the middle of a repair on my old motorcycle frame, when I realized I needed a reliable, steel-reinforced epoxy that could handle the metal stresses without fuss. I grabbed the J-B Weld Steel Reinforced Epoxy Syringe thinking it might just do the trick for that stubborn crack.
The syringe design makes it super easy to mix the two-part epoxy right at the site. The dark grey color blends nicely with steel, so I didn’t have to worry about it showing too much once dried.
I was impressed how smoothly it applied—no mess, no fuss—and it felt thick enough to stay put without dripping everywhere.
Once mixed, I pressed it into the crack and held it in place for a few minutes. The set time of 4-6 hours gave me enough flexibility to move onto other tasks without rushing.
I left it overnight, and by morning, it was rock solid. The strength is noticeable—this stuff really bonds to steel, holding firm under pressure and heat.
What I appreciated most was how well it handles high temperatures—up to 550°F. That’s perfect for automotive or marine repairs, where heat can be a real enemy.
After curing, I was able to drill, sand, and even file it with ease, making it versatile for finishing touches.
Overall, this epoxy feels like a trustworthy partner for heavy-duty repairs. It’s strong, durable, and easy to use.
If you need a steel-reinforced solution that works reliably, this syringe is definitely worth keeping on hand.
What Factors Should Be Considered When Choosing the Best Stick for Welding 1/8 Steel?
When choosing the best stick for welding 1/8 steel, several important factors must be considered to ensure a successful and strong weld.
- Electrode Type: The type of electrode determines the quality and characteristics of the weld. For 1/8 steel, commonly used electrodes include E6011, E6013, and E7018, each offering different penetration and deposition rates suitable for various applications.
- Welding Position: The position in which you will be welding (flat, horizontal, vertical, or overhead) impacts the choice of electrode. Some electrodes are designed for easier handling in specific positions, which can enhance control and reduce the chances of defects.
- Amperage Settings: The correct amperage is crucial for achieving a proper weld on 1/8 steel. Selecting a stick that matches the recommended amperage range for the chosen electrode will help in achieving optimal penetration and bead appearance.
- Heat Input: Managing heat input is essential to avoid warping or burning through the steel. Ensuring that the selected stick allows for controlled heat input will help maintain the integrity of the 1/8 steel while providing a strong weld.
- Material Composition: The composition of the steel being welded influences the choice of electrode. For low carbon steels, a mild steel electrode like E7018 is often preferred due to its ductility and strength, while for higher carbon steels, a different electrode may be necessary.
- Welding Environment: The conditions under which you are welding, such as wind or moisture, can affect the electrode’s performance. Choosing an electrode that is suitable for the specific environmental conditions will help ensure a quality weld.
- Ease of Use: The skill level of the welder also plays a role in the selection of the stick. Some electrodes are easier to work with than others, especially for beginners, making it important to consider the user’s experience when choosing.
How Does Amperage Influence Electrode Choice for 1/8 Steel?
- Electrode Diameter: The diameter of the electrode must match the amperage settings for optimal performance.
- Electrode Type: Different electrode types are suited for various applications and materials, influencing the choice based on the required strength and appearance of the weld.
- Welding Position: The position in which welding is performed can affect how amperage is applied and the resulting bead, thereby determining the best electrode choice.
- Welding Machine Settings: Proper settings on the welding machine, including amperage adjustment, are essential to ensure compatibility with the selected electrode.
Electrode Diameter: The diameter of the electrode should correlate with the amperage; generally, larger diameter electrodes can handle higher amperage and provide deeper penetration. For welding 1/8-inch steel, electrodes between 1/16-inch and 3/32-inch are commonly used, allowing for a balance of heat input and control.
Electrode Type: Common types of electrodes for stick welding include E6011, E6013, and E7018, each offering different characteristics like penetration and bead appearance. For 1/8-inch steel, E7018 is often favored for its strong welds and smooth finish, while E6011 can be used for dirty or rusty materials.
Welding Position: The position of the weld, whether flat, horizontal, vertical, or overhead, affects how the molten metal behaves and can influence the choice of electrode. Some electrodes perform better in specific positions and can help achieve the desired weld quality, making it necessary to consider the welding position when selecting an electrode.
Welding Machine Settings: Adjusting the welding machine settings to match the electrode and steel thickness is critical, as incorrect amperage can lead to undercutting or excessive spatter. For 1/8-inch steel, the recommended amperage range for E7018 typically falls between 70 to 100 amps, ensuring proper fusion and control with the selected electrode.
Why Is Base Metal Thickness Important in Electrode Selection?
Base metal thickness is crucial in electrode selection because it directly impacts the heat input, penetration, and fusion during the welding process. Selecting the appropriate electrode ensures that the weld pool can effectively melt the base metal, resulting in a strong and durable joint.
Research by the American Welding Society emphasizes that different electrodes are designed for specific metal thicknesses to optimize performance. For instance, when welding 1/8-inch thick steel, using an electrode with the right diameter and characteristics helps maintain the correct arc length and heat input, preventing issues like burn-through or insufficient penetration (AWS D1.1). This tailored approach is essential for achieving the desired mechanical properties in the weld.
The underlying mechanism involves the relationship between heat transfer and metal thickness. Thicker metals require more heat for adequate fusion, while thinner sections can be damaged by excessive heat. When an electrode is selected that matches the base metal thickness, the welder can control the heat application, allowing for the right amount of melting without compromising the integrity of the materials. This balance is critical in producing high-quality welds that meet structural standards and performance expectations.
What Types of Electrodes Are Most Effective for Welding 1/8 Steel?
The best stick electrodes for welding 1/8 inch steel include the following types:
- E6011: This electrode is known for its versatility and is effective in various positions, making it suitable for welding 1/8 inch steel, especially when dealing with dirty or rusty surfaces.
- E6013: E6013 electrodes are ideal for welding thin materials like 1/8 inch steel due to their smooth arc and minimal spatter, providing a clean finish that is often desired in aesthetic applications.
- E7014: This electrode offers excellent penetration and a stable arc, making it a great choice for welding 1/8 inch steel, particularly in flat and horizontal positions.
- E7018: Known for its high strength and low hydrogen content, E7018 is excellent for critical applications on 1/8 inch steel, providing a strong and ductile weld that resists cracking.
E6011: This electrode is highly effective for welding in all positions and can handle contaminated surfaces, which is a common scenario with 1/8 inch steel. It produces a deep penetration and is beneficial for connecting base metals with varying thicknesses, making it a reliable option for many welding projects.
E6013: E6013 electrodes are favored for their ease of use and excellent arc stability, which is particularly useful when welding thin sections like 1/8 inch steel. They produce a smooth, clean weld bead with less spatter, making it easier to achieve a visually appealing finish, which is why they are often preferred for light fabrication and maintenance work.
E7014: This type of electrode is designed for flat and horizontal welding and provides good penetration, making it suitable for 1/8 inch steel applications. It offers a stable arc and reduced spatter, making it easier for welders to control the weld pool and achieve consistent results.
E7018: E7018 electrodes are particularly valued in structural welding due to their low hydrogen content, which minimizes the risk of cracks in the weld. Their suitability for welding 1/8 inch steel lies in their ability to produce strong, ductile welds that can withstand stress, making them a top choice for critical applications and structural components.
Which Characteristics Make E6011 a Suitable Choice?
The characteristics that make E6011 a suitable choice for welding 1/8 inch steel include its versatility, penetration, and performance in various conditions.
- Good Penetration: E6011 electrodes are designed to provide deep penetration, which is crucial for welding thicker materials like 1/8 inch steel. This characteristic helps ensure that the weld is strong and can withstand stress without failing.
- Versatile Welding Positions: E6011 can be used in all positions, including flat, horizontal, vertical, and overhead. This versatility allows welders to tackle a variety of projects and scenarios without needing to switch electrodes.
- DC and AC Compatibility: E6011 can be used with both Direct Current (DC) and Alternating Current (AC) power sources. This flexibility means it can be utilized in different environments and setups, making it a practical choice for diverse welding applications.
- Excellent Arc Stability: This electrode provides a stable arc that makes it easier for welders to control the bead and produce consistent results. A stable arc reduces the risk of defects in the weld, contributing to a more aesthetically pleasing and strong joint.
- Good for Dirty or Rusty Surfaces: E6011 has the ability to weld through contaminants like rust, dirt, and oil. This characteristic is particularly useful when working with older or less maintained steel, as it allows for effective welding without extensive surface preparation.
What Advantages Does E7018 Offer for 1/8 Steel Welding?
The E7018 electrode is highly regarded for welding 1/8 inch steel due to its unique properties and performance advantages.
- Low Hydrogen Content: E7018 electrodes are designed to produce a low hydrogen weld deposit, which significantly reduces the risk of hydrogen-induced cracking in the weld bead. This is particularly important when welding high-strength steel and helps in achieving strong, durable joints.
- Excellent Arc Stability: The E7018 electrode provides a stable arc with minimal spatter, making it easier to control the weld pool. This stability allows for smoother and more precise welding, which is essential for achieving high-quality welds in thinner materials like 1/8 inch steel.
- Versatility: E7018 electrodes can be used in various positions (flat, horizontal, vertical, and overhead), making them versatile for different welding scenarios. This adaptability makes them a preferred choice for fabricators who need to work on multiple projects with varying orientations.
- Good Mechanical Properties: Welds made with E7018 electrodes exhibit excellent tensile strength and ductility. This means that the welds can withstand significant stress and are less likely to fail under load, which is crucial for structural applications involving 1/8 inch steel.
- Ease of Use: E7018 is relatively easy to use, even for novice welders, due to its forgiving nature and the ability to produce a clean weld with minimal cleanup required. This quality allows for quicker learning curves and increased productivity on the job site.
- Controlled Deposition Rate: The E7018 electrode offers a controlled deposition rate, which is beneficial when welding thinner materials. This helps prevent burn-through while ensuring adequate penetration and fusion of the steel being welded.
How Can You Optimize Your Welding Technique for 1/8 Steel?
Optimizing your welding technique for 1/8-inch steel requires attention to detail and proper equipment.
-
Select the Right Electrode: For welding 1/8 steel, a 6011 or 7018 electrode is ideal. These rods provide good penetration and a strong weld bead.
-
Adjust the Amperage: Set the welder’s amperage to between 90 and 130 amps, depending on the electrode diameter. Proper amperage ensures a clean bead without burning through the steel.
-
Maintain a Consistent Travel Speed: Move at a steady pace to promote uniform heat distribution. Too fast can lead to weak welds, while too slow may cause excessive buildup.
-
Use Proper Joint Preparation: Clean the steel surfaces to remove any rust, dirt, or oil. Proper fit-up of the joint also ensures strong fusion.
-
Control the Arc Length: Keeping a consistent arc length (about 1/16 inch) can minimize spatter and help maintain control.
-
Practice Technique: Employ techniques such as stringer beads for thicker sections and weave patterns for wider joints to enhance the strength of the weld.
Fine-tuning these aspects will significantly improve your welding efficiency and the quality of your seams on 1/8 steel.
What Techniques Enhance the Quality of Welds on 1/8 Steel?
There are several techniques that enhance the quality of welds on 1/8 steel, particularly when using stick welding methods.
- Proper Electrode Selection: Choosing the right type of electrode is crucial when welding 1/8 steel. For this thickness, electrodes like E6011 and E6013 are commonly recommended as they provide good penetration and a stable arc, helping to create strong welds.
- Adjusting Amperage Settings: Setting the correct amperage is essential for achieving optimal penetration and bead appearance. For 1/8 steel, an amperage range of 70 to 100 amps is typically effective, allowing the welder to maintain a steady travel speed without burning through the material.
- Maintaining a Consistent Travel Speed: A consistent travel speed is vital for uniform bead width and penetration. Too fast can lead to weak welds with poor fusion, while too slow can cause excessive heat input, leading to warping or burn-through.
- Controlling the Angle and Technique: The angle of the electrode should be maintained at about 15 to 30 degrees from vertical, which helps direct the heat into the base metal effectively. Techniques such as weaving or stringer beads can also be employed depending on the joint configuration and desired bead profile.
- Preheating the Material: Preheating the 1/8 steel can reduce the risk of cracking and improve the overall weld quality. This is especially helpful when dealing with thicker sections or when welding in colder environments, as it helps to maintain a more stable temperature during the welding process.
- Using Proper Joint Preparation: Cleaning the surface of the steel before welding can significantly enhance the quality of the weld. Removing contaminants like rust, oil, or mill scale ensures better fusion and reduces the likelihood of defects in the finished weld.
- Post-Weld Treatment: Implementing post-weld treatments, such as stress relieving or grinding down the welds, can enhance the overall integrity of the weld joint. This is particularly important when the welded structure will be subject to high stress or impact loads.
How Do Position and Angle Affect Joint Integrity?
Joint Fit-Up: Ensuring that the pieces being welded fit together correctly is essential for achieving a strong joint. Gaps or misalignments can lead to inconsistent penetration and increased likelihood of defects such as porosity or slag inclusions. A well-fitted joint allows for a more controlled weld pool and better fusion.
Travel Speed: The speed at which the welding torch or electrode is moved can drastically influence the heat input into the weld area. A slow travel speed can lead to excessive heat and distortion, while too fast a speed may not allow for proper penetration, both of which can result in weak joints. Balancing travel speed with other parameters is key to achieving a strong, durable weld.
What Safety Precautions Should Be Taken When Welding 1/8 Steel?
Proper Training equips welders with the knowledge to handle equipment safely and recognize potential hazards. It also ensures that they are familiar with emergency procedures, which is critical for addressing any incidents that may occur during the welding process.
What Personal Protective Equipment (PPE) is Essential for Welding?
The essential Personal Protective Equipment (PPE) for welding includes the following items:
- Welding Helmet: A welding helmet is crucial for protecting the face and eyes from intense light, ultraviolet (UV) rays, and harmful sparks. It typically features a dark filter lens to shield the welder from the bright arc and can have auto-darkening capabilities for convenience and safety.
- Flame-Resistant Clothing: Welders should wear flame-resistant clothing, such as jackets and pants made from materials like cotton or leather that resist ignition. This clothing helps protect against sparks, spatter, and heat, reducing the risk of burns and injuries during the welding process.
- Gloves: High-quality welding gloves are essential for hand protection from heat, sparks, and sharp metal edges. These gloves are usually made from leather or other durable materials that provide a good grip while allowing for flexibility and dexterity when handling welding equipment.
- Safety Boots: Steel-toed safety boots are important for protecting the feet from heavy objects that might fall during welding operations. They should also be made from flame-resistant materials to offer additional protection against sparks and molten metal.
- Respiratory Protection: Depending on the welding environment and materials being welded, a respirator may be necessary to protect against harmful fumes and gases. This can include a standard mask or a specialized respirator with filters designed to capture specific welding fumes.
- Ear Protection: In environments with loud welding equipment or processes, ear protection such as earplugs or earmuffs can help prevent hearing damage. This is particularly important in industrial settings where prolonged exposure to noise is common.
- Face Shield: In addition to a helmet, a face shield provides extra protection for the face against flying debris and sparks. It is often used in conjunction with safety goggles to ensure comprehensive coverage of the facial area.
What Common Mistakes Should Be Avoided to Ensure Successful Welding of 1/8 Steel?
To ensure successful welding of 1/8 steel, it is crucial to avoid common mistakes that can compromise the integrity of the weld.
- Using Incorrect Electrode: Selecting the wrong type of electrode can lead to poor penetration and weak welds. For 1/8 steel, low hydrogen electrodes, such as E7018, are often recommended as they provide better strength and ductility.
- Poor Fit-Up: Inadequate preparation of the materials being welded can create gaps and misalignments. Proper fit-up ensures that the weld pool can flow uniformly, resulting in a stronger bond and less likelihood of defects.
- Improper Welding Technique: Using incorrect angles or travel speeds can lead to inconsistent bead profiles and inadequate fusion. Maintaining a steady hand and appropriate speed will help achieve a uniform weld and minimize issues like undercutting or overlap.
- Neglecting Cleanliness: Dirt, oil, or rust on the steel surface can hinder the welding process. It’s essential to clean the surfaces thoroughly to ensure proper fusion and avoid contamination that can weaken the weld.
- Inadequate Heat Settings: Setting the amperage too low can result in insufficient penetration, while too high can cause burn-through. Adjusting the heat settings according to the material thickness and electrode type is vital for achieving the optimal weld quality.
- Ignoring Safety Precautions: Failing to wear appropriate protective gear can lead to serious injuries. Always use gloves, a welding helmet, and protective clothing to guard against sparks and harmful radiation during the welding process.
- Insufficient Post-Weld Treatment: Neglecting to treat the weld after completion can lead to premature failure. Post-weld cleaning and inspection are crucial to identify any defects and ensure the integrity of the weld.
How Can Poor Technique Impact Your Welding Results?
Poor technique can severely impact welding results, leading to defects and compromising the integrity of the weld.
- Inconsistent Arc Length: Maintaining a proper arc length is crucial for effective welding. A too-long arc can lead to excessive spatter and poor penetration, while a too-short arc can cause the electrode to stick, leading to a failed weld.
- Improper Travel Speed: The speed at which the welder moves the electrode affects the weld bead’s shape and quality. Moving too fast can result in weak, undercut welds, while moving too slowly can create excessive heat, leading to distortion and burn-through.
- Incorrect Electrode Angle: The angle at which the electrode is held can influence the weld bead’s profile and penetration. An incorrect angle can lead to uneven deposition of filler material, which may cause weak spots or defects in the weld.
- Inadequate Cleaning of Base Material: Contaminants on the base material, such as rust, oil, or paint, can hinder the welding process. Properly cleaning the surfaces to be welded ensures good fusion and prevents inclusions that can weaken the weld.
- Improper Electrode Selection: Choosing the wrong electrode for the specific type of steel being welded can lead to poor results. For example, using a low-quality stick electrode on 1/8 steel may result in inadequate penetration or excessive slag, while using the best stick for this thickness can ensure a strong, clean weld.
What Are the Consequences of Using Incorrect Electrode Types?
The consequences of using incorrect electrode types can significantly impact the quality of the weld and the integrity of the material being welded.
- Poor Weld Quality: Using the wrong electrode can lead to insufficient penetration and inconsistent bead appearance. This results in a weak joint that may not hold under stress or load.
- Increased Porosity: Incorrect electrodes can introduce contaminants or cause improper shielding, leading to porosity in the weld. This diminishes the mechanical properties of the weld and can create points of failure.
- Incompatibility with Base Material: Some electrodes are not designed for specific materials, which can lead to poor adhesion and joint failure. When welding 1/8 steel, using the right electrode ensures compatibility and optimal bonding.
- Excessive Spatter: Using an unsuitable electrode may lead to increased spatter during the welding process. This not only affects the appearance of the weld but requires additional cleanup and can also cause defects in the final product.
- Weld Cracking: Improperly chosen electrodes may result in thermal stresses that lead to cracking in the weld or base material. This is particularly critical in situations where structural integrity is paramount.
- Increased Work Time: Using the wrong electrode can result in more time spent fixing defects, reworking welds, or cleaning up spatter. This inefficiency increases labor costs and extends project timelines.