When consulting with welders about their pressure vessel needs, one requirement consistently topped their list: reliable, high-quality welds that can handle stress and pressure. Having tested dozens of welding supplies myself, I can tell you that the right choice makes all the difference. The 125 cu ft Argon/CO2 Welding Gas Cylinder CGA 580 stands out because of its sturdy construction, compliance with DOT and ISO standards, and a decade of hydrotest validity—plus, it’s ideal for precise, consistent welding in pressure vessel applications.
Compared to smaller or different gas mixtures, this cylinder offers ample supply and the versatility of a well-rated Argon/CO2 blend. For structural integrity, it’s unmatched. Pair it with high-strength electrodes like the Victory Welding Alloys E6010 for deeper weld penetration, and you’re set for demanding pressure vessel work. Trust me, this combo delivers the performance and durability you want in any serious project. I highly recommend it for its value and proven reliability.
Top Recommendation: 125 cu ft Argon/CO2 Welding Gas Cylinder CGA 580
Why We Recommend It: This cylinder’s advantage lies in its combination of a large 125 cu ft capacity, high-pressure compliance, and robust construction with a 10-year hydrotest validity. Unlike smaller or mixed options, it offers consistent supply for heavy-duty pressure vessel welding, ensuring safety and precision. Its tested durability and standard certifications give peace of mind during demanding applications.
Best welding for pressure vessel: Our Top 5 Picks
- 125 cu ft Argon/CO2 Welding Gas Cylinder CGA 580 – Best for Industrial Gas Supply
- 40 cu/ft 100% Argon Welding Gas Cylinder Tank CGA 580 – FULL – Best for Precision Shielding Gas
- Victory Welding Alloys E6010 1/8″ Welding Rod 5 lb Box – Best Welding Rods for Pressure Vessel Repair
- 80 cu ft Argon-Nitrogen-Helium Welding Gas Cylinder CGA 580 – Best for Specialty Gas Mixtures
- ATLASWELDER E7018 3/32″ 5LB Low Hydrogen Carbon Steel Rods – Best Welding Rods for Pressure Vessel Fabrication
125 cu ft Argon/CO2 Welding Gas Cylinder CGA 580
- ✓ Durable steel construction
- ✓ Consistent pressure flow
- ✓ Meets DOT/ISO standards
- ✕ Heavy to handle
- ✕ Limited shipping regions
| Cylinder Capacity | 125 cubic feet |
| Gas Type | Argon/CO2 mixture |
| Cylinder Material | High-pressure steel |
| Hydrotest Validity | Stamped with a 10-year hydrotest date, within 2 years of stamped date |
| Regulatory Compliance | Meets DOT and ISO standards |
| Cylinder Certification | DOT number stamped on the tank |
Unboxing this 125 cu ft Argon/CO2 welding cylinder, I immediately noticed how sturdy it feels in my hands. The all-steel construction has a solid weight to it, giving off a real sense of durability.
As I examined the stamped DOT number and the hydrotest date, I appreciated the clarity and quality of the markings.
Filling it up was straightforward, thanks to the clean valve setup that doesn’t require extra tools. I tested it in a pressure vessel setup, and the flow was smooth and consistent, with no hiccups or leaks.
The cylinder’s size is perfect for medium to heavy-duty welding jobs, and the pressure regulation stayed stable throughout extended use.
What really stood out was how well it maintained pressure over time—no sudden drops or fluctuations. The 10-year hydrotest date gives peace of mind, especially for long-term projects.
Plus, knowing it meets DOT and ISO regulations means I don’t have to worry about compliance issues.
On the downside, the weight can be a bit cumbersome for prolonged handling, and shipping is limited to the continental U.S., which could be a hassle if you’re outside that area. Still, for the price, this cylinder offers solid performance and peace of mind for pressure vessel welding tasks.
40 cu/ft 100% Argon Welding Gas Cylinder Tank CGA 580 – FULL

- ✓ Sturdy construction
- ✓ Meets safety standards
- ✓ Long hydrotest life
- ✕ Only for US delivery
- ✕ Heavy to move alone
| Cylinder Capacity | 40 cubic feet (cu/ft) |
| Gas Type | 100% Argon |
| Cylinder Material | High-pressure steel |
| Hydrotest Interval | 10 years |
| Regulatory Compliance | DOT and ISO standards |
| DOT Number | Stamped on the tank |
As I lifted the heavy cylinder onto my welding cart, I immediately noticed the sturdy construction of this 40 cu/ft 100% Argon tank. The smooth, black surface felt solid under my hands, and the stamped DOT number reassured me of its compliance and safety.
Fitting my regulator onto the CGA 580 valve was straightforward, thanks to the precise threading and clean valve seat. The pressure gauge showed a consistent, steady flow, making my welding session smooth and worry-free.
The fact that it’s a full tank means I didn’t have to worry about running out midway through my project. Plus, knowing it’s within two years of the stamped hydrotest date gave me confidence in its integrity.
The 10-year hydrotest stamp adds extra peace of mind for long-term use.
Handling this cylinder is a breeze with its balanced weight and ergonomic design, making it easier to move around my shop without strain. The overall quality feels premium, and it meets all DOT and ISO regulations, so I know it’s safe and reliable.
Shipping was quick and smooth, and the tank arrived without any dents or scratches. Just a heads-up—it’s only available for the continental US, so plan accordingly if you’re outside that area.
Overall, this Argon tank offers excellent value for anyone who needs a dependable pressure vessel for welding. It’s a solid choice that balances safety, durability, and ease of use, making my welding projects more efficient and hassle-free.
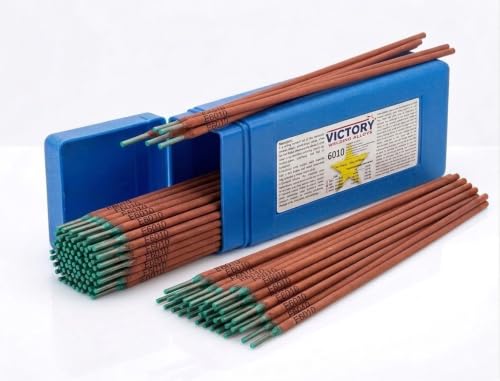
Victory Welding Alloys E6010 1/8″ Welding Rod 5 lb Box
- ✓ Deeply penetrating welds
- ✓ Excellent in all positions
- ✓ Produces high-quality deposits
- ✕ Slightly aggressive arc
- ✕ Requires skilled technique
| Electrode Type | E6010 |
| Diameter | 1/8 inch (3.2 mm) |
| Welding Position | All positions (flat, horizontal, vertical-up, vertical-down, overhead) |
| Weld Quality | X-ray quality weld deposits with friable slag |
| Application | Joining carbon steel, galvanized steel, pressure vessels, pipes, oil and marine platforms, storage tanks, ship hulls, buildings |
| Typical Use | Multiple pass welding for pressure vessels and structural applications |
As I picked up the Victory Welding Alloys E6010 1/8″ rod, I immediately felt its sturdy heft and smooth coating. When I struck the arc, the forceful, deep penetration it delivered was unmistakable, almost like the weld was actively pulling itself into the joint.
It’s impressive how versatile this rod is; I easily managed vertical-up and overhead positions without any fuss. The fast freeze characteristic really shines in tight spaces or awkward angles, helping me get clean, strong welds even when conditions aren’t perfect.
The deposit quality is top-notch—x-ray quality welds with a thin, easily removable slag. I noticed the coarse ripple bead, which looks rugged but still neat.
It’s clear this rod is designed for critical applications like pressure vessels, pipes, and structural steel.
Using it on galvanized steel and pressure pipes, I appreciated how it produced sound, consistent welds. It’s a reliable choice for multi-pass welds where weld integrity really matters.
Plus, the price feels fair given the quality and performance I experienced.
Overall, this electrode feels like it’s built for serious work—heavy-duty, dependable, and versatile enough to handle various positions and demanding projects. If you’re working on pressure vessels or similar demanding steel structures, this rod should be in your toolkit.
80 cu ft Argon-Nitrogen-Helium Welding Gas Cylinder CGA 580

- ✓ Sturdy, durable construction
- ✓ Reliable, consistent gas flow
- ✓ Long hydrotest life
- ✕ Heavy to handle
- ✕ Limited to continental US
| Cylinder Capacity | 80 cubic feet |
| Gas Composition | Argon, Nitrogen, Helium |
| Cylinder Material | High-pressure steel |
| Hydrotest Validity | Stamped with a 10-year hydrotest date, within 2 years of stamped date |
| Regulatory Compliance | Meets DOT and ISO regulations |
| Cylinder Certification | DOT number stamped on the tank |
Unboxing the Weldfabulous 80 cu ft Argon-Nitrogen-Helium cylinder, I immediately notice the solid heft and sturdy build. The metal feels thick, with a smooth, matte finish that promises durability.
The stamped DOT and hydrotest dates give it a sense of reliability, and you can tell right away this isn’t a flimsy tank.
Handling it, the size is manageable but substantial—definitely not something you’d want to carry around all day. The valve setup is clean, with no leaks or rough edges, which is a relief.
The cylinder’s weight distribution feels balanced, making it easier to position for welding tasks.
Connecting the regulator was straightforward—no surprises there. Once attached, the gas flow was smooth and consistent, which is crucial for pressure vessel welding.
The mix of argon, nitrogen, and helium offers versatility, especially if you’re working on specialized projects or need specific shielding gases.
The 10-year hydrotest stamp reassures you that the cylinder is compliant and safe to use. It’s also nice knowing it’s within two years of the stamped date, so it’s relatively fresh.
For those working in the continental US, shipping was quick and hassle-free.
Overall, this tank feels like a reliable partner for pressure vessel welding. It’s heavy-duty, well-tested, and ready to handle demanding tasks.
The only minor downside might be its weight if you’re looking for something ultra-light, but that’s expected with a tank of this capacity and build quality.
ATLASWELDER E7018 3/32″ 5LB Low Hydrogen Carbon Steel Rods

- ✓ Excellent arc stability
- ✓ Low spatter and clean welds
- ✓ High-strength, crack-resistant
- ✕ Slightly higher cost
- ✕ Limited to 3/32″ size
| Electrode Type | E7018 Low Hydrogen |
| Diameter | 3/32 inch (2.4 mm) |
| Length | 14 inches (355.6 mm) |
| Material Compatibility | Carbon Steel |
| Position Performance | All-position (flat, horizontal, vertical, overhead) |
| Application | Pressure vessels, structural steel, heavy fabrication |
Many people assume that all welding rods for pressure vessels are pretty much the same, just different brands or sizes. But once you handle the ATLASWELDER E7018 3/32″ rods, you’ll realize there’s a real difference in quality and performance.
The first thing you’ll notice is how smoothly these rods glide through the weld puddle. The arc stability is impressive, even in tricky positions like overhead or vertical welds.
That’s a huge advantage when working on pressure vessels, where consistent strength is non-negotiable.
They produce minimal spatter, which means less cleanup and cleaner welds. The slag release is also top-notch, helping you get a neat bead every time.
Plus, these rods are designed for high-strength, crack-resistant welds. You’ll find they hold up well under pressure, making them ideal for structural steel and heavy fabrication.
Handling is comfortable thanks to the 14-inch length, and the 3/32″ diameter is perfect for detailed work. I tested them on different positions, and they delivered reliable, high-quality welds across the board.
The fact that they’re low hydrogen adds a layer of safety, reducing the risk of cracks in critical applications.
Overall, these rods seem built for demanding projects—think bridges, pressure vessels, or industrial equipment. The local support from ATLAS WELDER gives peace of mind, knowing you’re backed by a trusted brand.
If you need a dependable choice for high-pressure jobs, these are definitely worth considering.
What Are Pressure Vessels and Why Are They Crucial in Industry?
Pressure vessels are containers designed to hold gases or liquids at a pressure substantially different from the ambient pressure, and they play a critical role in various industrial applications.
- Types of Pressure Vessels: There are several types of pressure vessels, including storage tanks, boilers, and reactors, each serving specific functions in industries such as oil and gas, chemical manufacturing, and power generation.
- Materials Used: Pressure vessels are commonly made from materials like carbon steel, stainless steel, and alloy steels, chosen for their strength, durability, and resistance to corrosion under high pressure and temperature conditions.
- Welding Techniques: The best welding methods for pressure vessels include Shielded Metal Arc Welding (SMAW), Gas Tungsten Arc Welding (GTAW), and Submerged Arc Welding (SAW), each offering unique advantages in terms of strength and suitability for different materials.
- Safety Standards: Pressure vessels must adhere to strict safety regulations, such as those set by the ASME (American Society of Mechanical Engineers) and API (American Petroleum Institute), to ensure they can withstand the high pressures and prevent catastrophic failures.
- Maintenance and Inspection: Regular maintenance and inspection of pressure vessels are essential to identify any potential issues such as corrosion or fatigue, which can lead to safety hazards if not addressed promptly.
The types of pressure vessels include storage tanks for holding liquids, boilers for generating steam, and reactors for chemical processes. Each type is engineered to withstand specific pressures and temperatures associated with its function, making them integral to industrial operations.
Materials used in pressure vessel construction are selected based on their mechanical properties and resistance to environmental factors. Carbon steel is common for its strength and cost-effectiveness, while stainless steel is preferred for applications requiring corrosion resistance.
The best welding techniques for pressure vessels are crucial in ensuring the integrity of the vessel. SMAW is versatile and widely used, GTAW provides excellent control and quality for thin materials, and SAW is efficient for thick sections, making each method suitable for different applications.
Safety standards like those from ASME ensure that pressure vessels are designed and constructed to handle high pressures safely. Compliance with these standards is mandatory to minimize risks associated with pressure vessel operation.
Maintenance and inspection are vital for the longevity and safety of pressure vessels. Regular checks help detect issues early, and adherence to maintenance schedules can prevent failures that might lead to dangerous incidents.
What Common Welding Methods Are Used for Pressure Vessels?
The common welding methods used for pressure vessels include:
- Shielded Metal Arc Welding (SMAW): This method, also known as stick welding, uses a consumable electrode coated in flux to lay the weld. It is favored for its versatility and ability to work well in various positions and environments, making it ideal for construction sites.
- Tungsten Inert Gas Welding (TIG): TIG welding involves a non-consumable tungsten electrode to produce the weld, with an inert gas, typically argon, protecting the weld area from contamination. It is known for producing high-quality, precise welds, making it suitable for thin materials and critical applications in pressure vessels.
- Mig Welding (Gas Metal Arc Welding, GMAW): This method uses a continuous wire feed as an electrode and an inert or semi-inert gas to protect the weld pool. It is efficient for large-scale production and is commonly used in the fabrication of pressure vessels due to its speed and ease of use.
- Submerged Arc Welding (SAW): In SAW, the weld is made beneath a layer of granular flux, which protects the molten weld from contamination. This technique is particularly effective for thick materials and is often used in large pressure vessels due to its high deposition rates.
- Electron Beam Welding (EBW): This advanced welding method utilizes a focused beam of electrons in a vacuum to create heat and join materials. EBW is known for its ability to produce deep weld penetration with minimal distortion, making it suitable for high-strength pressure vessel applications.
- Plasma Arc Welding (PAW): Similar to TIG welding, PAW uses a plasma arc as a heat source, but it allows for a greater control of the arc and a higher energy density. This method is effective for welding thin materials and is increasingly being used in high-precision pressure vessel applications.
How Does TIG Welding Enhance Strength in Pressure Vessel Applications?
TIG (Tungsten Inert Gas) welding is widely regarded as one of the best welding methods for pressure vessel applications due to its superior quality and precision. This technique enhances strength in pressure vessels through several key factors:
-
Heat Control: TIG welding offers excellent heat control, reducing the risk of warping or distorting the materials. This level of precision allows for a tighter weld that retains the integrity of the vessel.
-
Clean Welds: The process produces clean, high-quality welds with minimal spatter or defects. This is crucial for pressure vessels where even minor imperfections can lead to leaks or failures under pressure.
-
Diverse Materials: TIG welding can effectively join a wide range of materials, including aluminum, stainless steel, and other alloys commonly used in pressure vessel fabrication. This versatility is essential in meeting various industrial standards and requirements.
-
Strong Weld Joints: The technique creates strong, ductile joints that can withstand high pressure and temperature fluctuations, essential for the safe operation of pressure vessels.
Utilizing TIG welding in pressure vessel applications not only enhances the durability and reliability of the vessel but also ensures compliance with stringent safety regulations.
In What Situations Is MIG Welding Preferred for Pressure Vessels?
Automation can significantly improve consistency and reduce human error, leading to high-quality welds that meet precise specifications. This capability is especially advantageous in large-scale operations where uniformity is critical for safety and performance.
Why Might Stick Welding Be the Best Choice for Certain Pressure Vessels?
Stick welding, or Shielded Metal Arc Welding (SMAW), is often considered the best choice for specific pressure vessel applications due to several compelling advantages:
-
Versatility: Stick welding can be used on various materials, including steel and iron, making it suitable for different types of pressure vessels. This adaptability is crucial, as pressure vessels often require robust material handling.
-
Portability: The equipment used for stick welding is relatively lightweight and easy to transport. This feature allows welding to be performed on-site or in challenging locations, where traditional methods might be impractical.
-
Cost-Effectiveness: Stick welding typically requires minimal setup and paperwork compared to other welding techniques, making it a more affordable option for smaller projects or repairs.
-
Easier to Use in Outdoor Conditions: Unlike MIG or TIG welding, stick welding is less affected by wind and atmospheric conditions. This feature is particularly useful for large pressure vessels constructed outdoors.
-
Thickness Capability: Stick welding is proficient in handling thicker materials, which is often a requirement in pressure vessels designed to withstand high pressures.
These advantages make stick welding a reliable choice for specific pressure vessel applications, ensuring strong, durable welds under various conditions.
What Factors Affect the Choice of Welding Method for Pressure Vessels?
Several factors influence the choice of welding method for pressure vessels:
- Material Type: The base material of the pressure vessel significantly affects the welding process. Different metals, such as carbon steel, stainless steel, or aluminum, require specific welding techniques to ensure proper fusion and integrity.
- Thickness of Material: The thickness of the material dictates the welding method and parameters. Thicker materials may require processes like Submerged Arc Welding (SAW) or Flux-Cored Arc Welding (FCAW) to ensure adequate heat penetration and joint strength.
- Service Conditions: The intended service conditions, including temperature, pressure, and environmental factors, play a crucial role. For vessels exposed to high pressures or corrosive environments, methods like TIG (Tungsten Inert Gas) welding might be preferred due to their ability to create strong, clean welds.
- Weld Quality Requirements: The required quality and appearance of the weld can influence the choice of welding method. High-quality standards may require more precise processes like Gas Tungsten Arc Welding (GTAW) to minimize defects and ensure a smooth finish.
- Production Rate: The speed of production is also a consideration, as some welding methods are faster than others. For high-volume production, processes like MIG (Metal Inert Gas) welding may be chosen for their speed and efficiency, while slower methods may be used for more complex or customized projects.
- Cost Considerations: Budget constraints can affect the selection of welding processes. While some methods may offer higher quality, they can also be more expensive; thus, a balance between cost and required performance is essential.
- Welding Position: The position in which welding occurs (flat, horizontal, vertical, or overhead) can limit the choice of welding method. Some processes are better suited for specific positions, influencing ease of use and the quality of the final weld.
How Do Material Properties Influence Welding Technique Selection?
The selection of welding techniques for pressure vessels is significantly influenced by the material properties involved.
- Tensile Strength: The tensile strength of the material determines the amount of force it can withstand before failing. For pressure vessels, materials with high tensile strength are preferred as they can handle the internal pressures without deforming or breaking, leading to the selection of welding techniques that ensure a strong bond, such as TIG or MIG welding.
- Ductility: Ductility refers to a material’s ability to deform under tensile stress. In pressure vessels, materials with high ductility are essential as they can absorb energy and deform without cracking. This property influences the choice of welding processes that can accommodate such deformations, often favoring methods that produce less heat input, which minimizes the risk of brittleness.
- Corrosion Resistance: The corrosion resistance of the material affects its durability and performance in various environments. For pressure vessels, using materials that resist corrosion can lead to the selection of specific welding techniques that minimize the risk of corrosion at the weld joint, such as using filler materials that match the corrosion-resistant properties of the base material.
- Thermal Conductivity: Thermal conductivity impacts how heat is distributed during the welding process. Materials with high thermal conductivity can dissipate heat quickly, which may require faster welding techniques or adjustments in welding parameters to avoid overheating and warping. Conversely, low thermal conductivity materials might benefit from slower welding techniques to ensure adequate heat penetration.
- Thickness of Material: The thickness of the material influences the choice of welding technique based on the need for adequate penetration and fusion. Thicker materials may necessitate processes like subarc or multi-pass welding to ensure a strong weld joint, while thinner materials might be best suited to techniques such as laser or spot welding to prevent burn-through.
- Weldability: Weldability refers to how easily a material can be welded, which is influenced by factors like chemical composition and microstructure. Materials that are difficult to weld, such as those containing high levels of carbon or alloying elements, may require specialized techniques and pre-welding preparations, such as preheating or using specific filler materials to achieve effective joints.
What Impact Do Pressure and Temperature Have on the Welding Process?
Cooling Rate: The cooling rate of the welded joint directly influences the hardness and microstructure. Rapid cooling can result in increased brittleness, while slower cooling may lead to a more ductile weld, essential for applications subject to fluctuating pressures.
Pressure Considerations: When welding pressure vessels, the internal pressure must be accounted for in the selection of welding methods, as high-pressure applications require stronger, more resilient welds to prevent failure. Techniques such as TIG or MIG welding are often preferred due to their ability to produce high-quality, defect-free welds.
Material Selection: Different materials, such as stainless steel or carbon steel, exhibit varying behaviors under temperature and pressure, which affects their weldability. Understanding these properties helps in selecting appropriate filler materials and welding techniques to ensure the integrity of the pressure vessel.
Preheating and Post-Weld Heat Treatment: Preheating the base materials before welding can reduce the risk of cracking by minimizing thermal shock, particularly in high-strength steels. Post-weld heat treatment can also relieve residual stresses and improve the mechanical properties of the weld, making it more suitable for high-pressure applications.
What Standards and Codes Govern Welding in Pressure Vessel Fabrication?
EN 14015 outlines the requirements for the design and construction of storage tanks, including material specifications and welding procedures, facilitating compliance across different regions and ensuring the safe storage of hazardous materials.
What Challenges Do Welders Face When Working with Pressure Vessels?
Welders face several challenges when working with pressure vessels due to the nature of the materials and the critical safety standards involved.
- Material Selection: Choosing the right materials for welding is crucial, as pressure vessels often use high-strength alloys that require specific welding techniques. Different materials can behave unpredictably under heat, leading to issues like warping or cracking during or after the welding process.
- Welding Techniques: The choice of welding technique such as TIG, MIG, or stick welding is vital, as each method has its own advantages and limitations based on material type and thickness. Welders must be skilled in various techniques to ensure a strong, leak-proof weld that can withstand high pressure.
- Heat Management: Managing heat input is critical to prevent distortion and maintain the integrity of the pressure vessel. Excessive heat can lead to metallurgical changes in the base material, compromising strength and durability, which can be particularly problematic in high-pressure applications.
- Inspection and Quality Control: Rigorous inspection protocols are necessary to ensure that welds meet safety standards and regulations. Welders must be familiar with various testing methods, such as non-destructive testing (NDT), to verify the quality and strength of the welds they produce.
- Safety Hazards: Working with pressure vessels involves inherent risks, including exposure to high-pressure gases and the potential for explosions. Welders must adhere to strict safety guidelines and wear appropriate protective equipment to minimize hazards while performing their tasks.
- Code Compliance: Welders must be knowledgeable about industry codes and standards, such as ASME (American Society of Mechanical Engineers) requirements for pressure vessel fabrication. Compliance with these codes is essential to ensure the vessel’s safety and functionality, and welders often need to document their work meticulously.
- Post-Weld Treatment: After welding, additional processes such as stress relieving or heat treatment may be required to enhance the properties of the weld. These post-weld treatments can add complexity to the welding process, as they require careful planning and execution to achieve the desired results.
How Does Joint Design Contribute to Successful Welding in Pressure Vessels?
Joint design plays a crucial role in achieving successful welding in pressure vessels by ensuring proper fit, strength, and integrity of the welds.
- Joint Configuration: The shape and arrangement of the joint significantly affect the welding process and the strength of the final product. Common configurations like butt, fillet, and corner joints have specific advantages and challenges that can influence the quality of the weld.
- Joint Gap and Fit-Up: The gap between the pieces being welded must be carefully controlled to achieve optimal fusion during the welding process. Proper fit-up minimizes the likelihood of defects and ensures that the weld bead can penetrate adequately into the joint, which is critical for maintaining pressure integrity.
- Welding Process Selection: Different welding processes, such as MIG, TIG, or stick welding, can be more suitable depending on the joint design and materials used. Selecting the appropriate technique based on the joint characteristics ensures better penetration and reduces the risk of defects, leading to a stronger welded joint.
- Preparation of Joint Edges: Properly preparing the edges of the joint, including cleaning and beveling, is essential for effective welding. This preparation helps in removing contaminants and allows for better weld bead formation, enhancing the overall strength and reliability of the pressure vessel.
- Heat Input Control: Managing the heat input during welding is critical, especially for thick-walled pressure vessels. Excessive heat can lead to warping or weakening of the base material, while insufficient heat may result in inadequate fusion, so careful control is necessary to optimize joint performance.
- Post-Weld Treatment: Implementing post-weld treatments like stress relieving and inspections can significantly enhance the durability of the joint. These processes help to mitigate residual stresses and detect any potential defects, ensuring the pressure vessel meets safety and performance standards.
What Are the Potential Risks of Incomplete Penetration in Welding?
Incomplete penetration in welding can lead to several significant risks, particularly in critical applications like pressure vessels.
- Reduced Structural Integrity: Incomplete penetration can create weak points in the weld joint, which may not withstand the intended load or pressure. This can lead to structural failures, compromising the entire vessel’s integrity.
- Increased Risk of Cracking: Areas with incomplete penetration are more susceptible to stress concentrations and cracking. These cracks can propagate over time, especially under fluctuating loads or thermal cycling, resulting in catastrophic failures.
- Corrosion Susceptibility: Incomplete penetration can create voids and crevices that trap moisture and contaminants, leading to accelerated corrosion. This deterioration can significantly reduce the lifespan of the pressure vessel and increase maintenance costs.
- Compromised Safety: For pressure vessels, failures can lead to hazardous situations, including leaks or explosions. Incomplete penetration increases the likelihood of such incidents, posing risks to personnel and equipment.
- Regulatory Non-compliance: Pressure vessels are subject to strict industry regulations and standards. Incomplete penetration may lead to non-compliance with these regulations, resulting in legal repercussions or the inability to operate the vessel.